

[facilities]
Every process your part needs, in our own plants
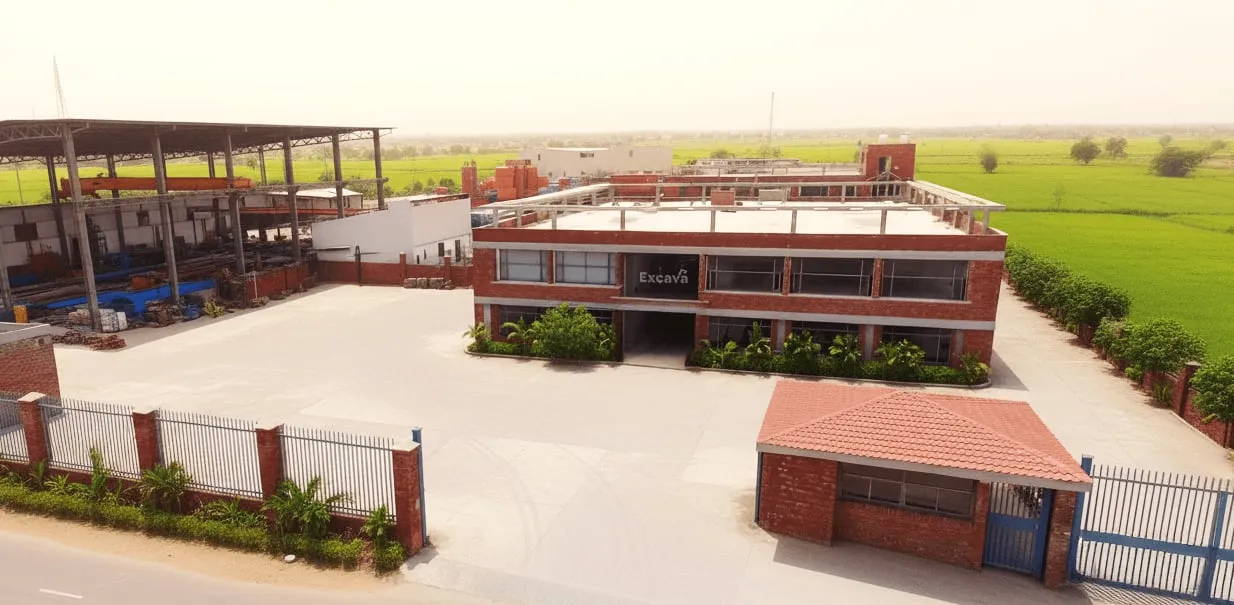
From the first laser cut to final assembly, 15 processes across two plants in Palwal, Delhi NCR. Your parts stay with one team from cutting to shipping.
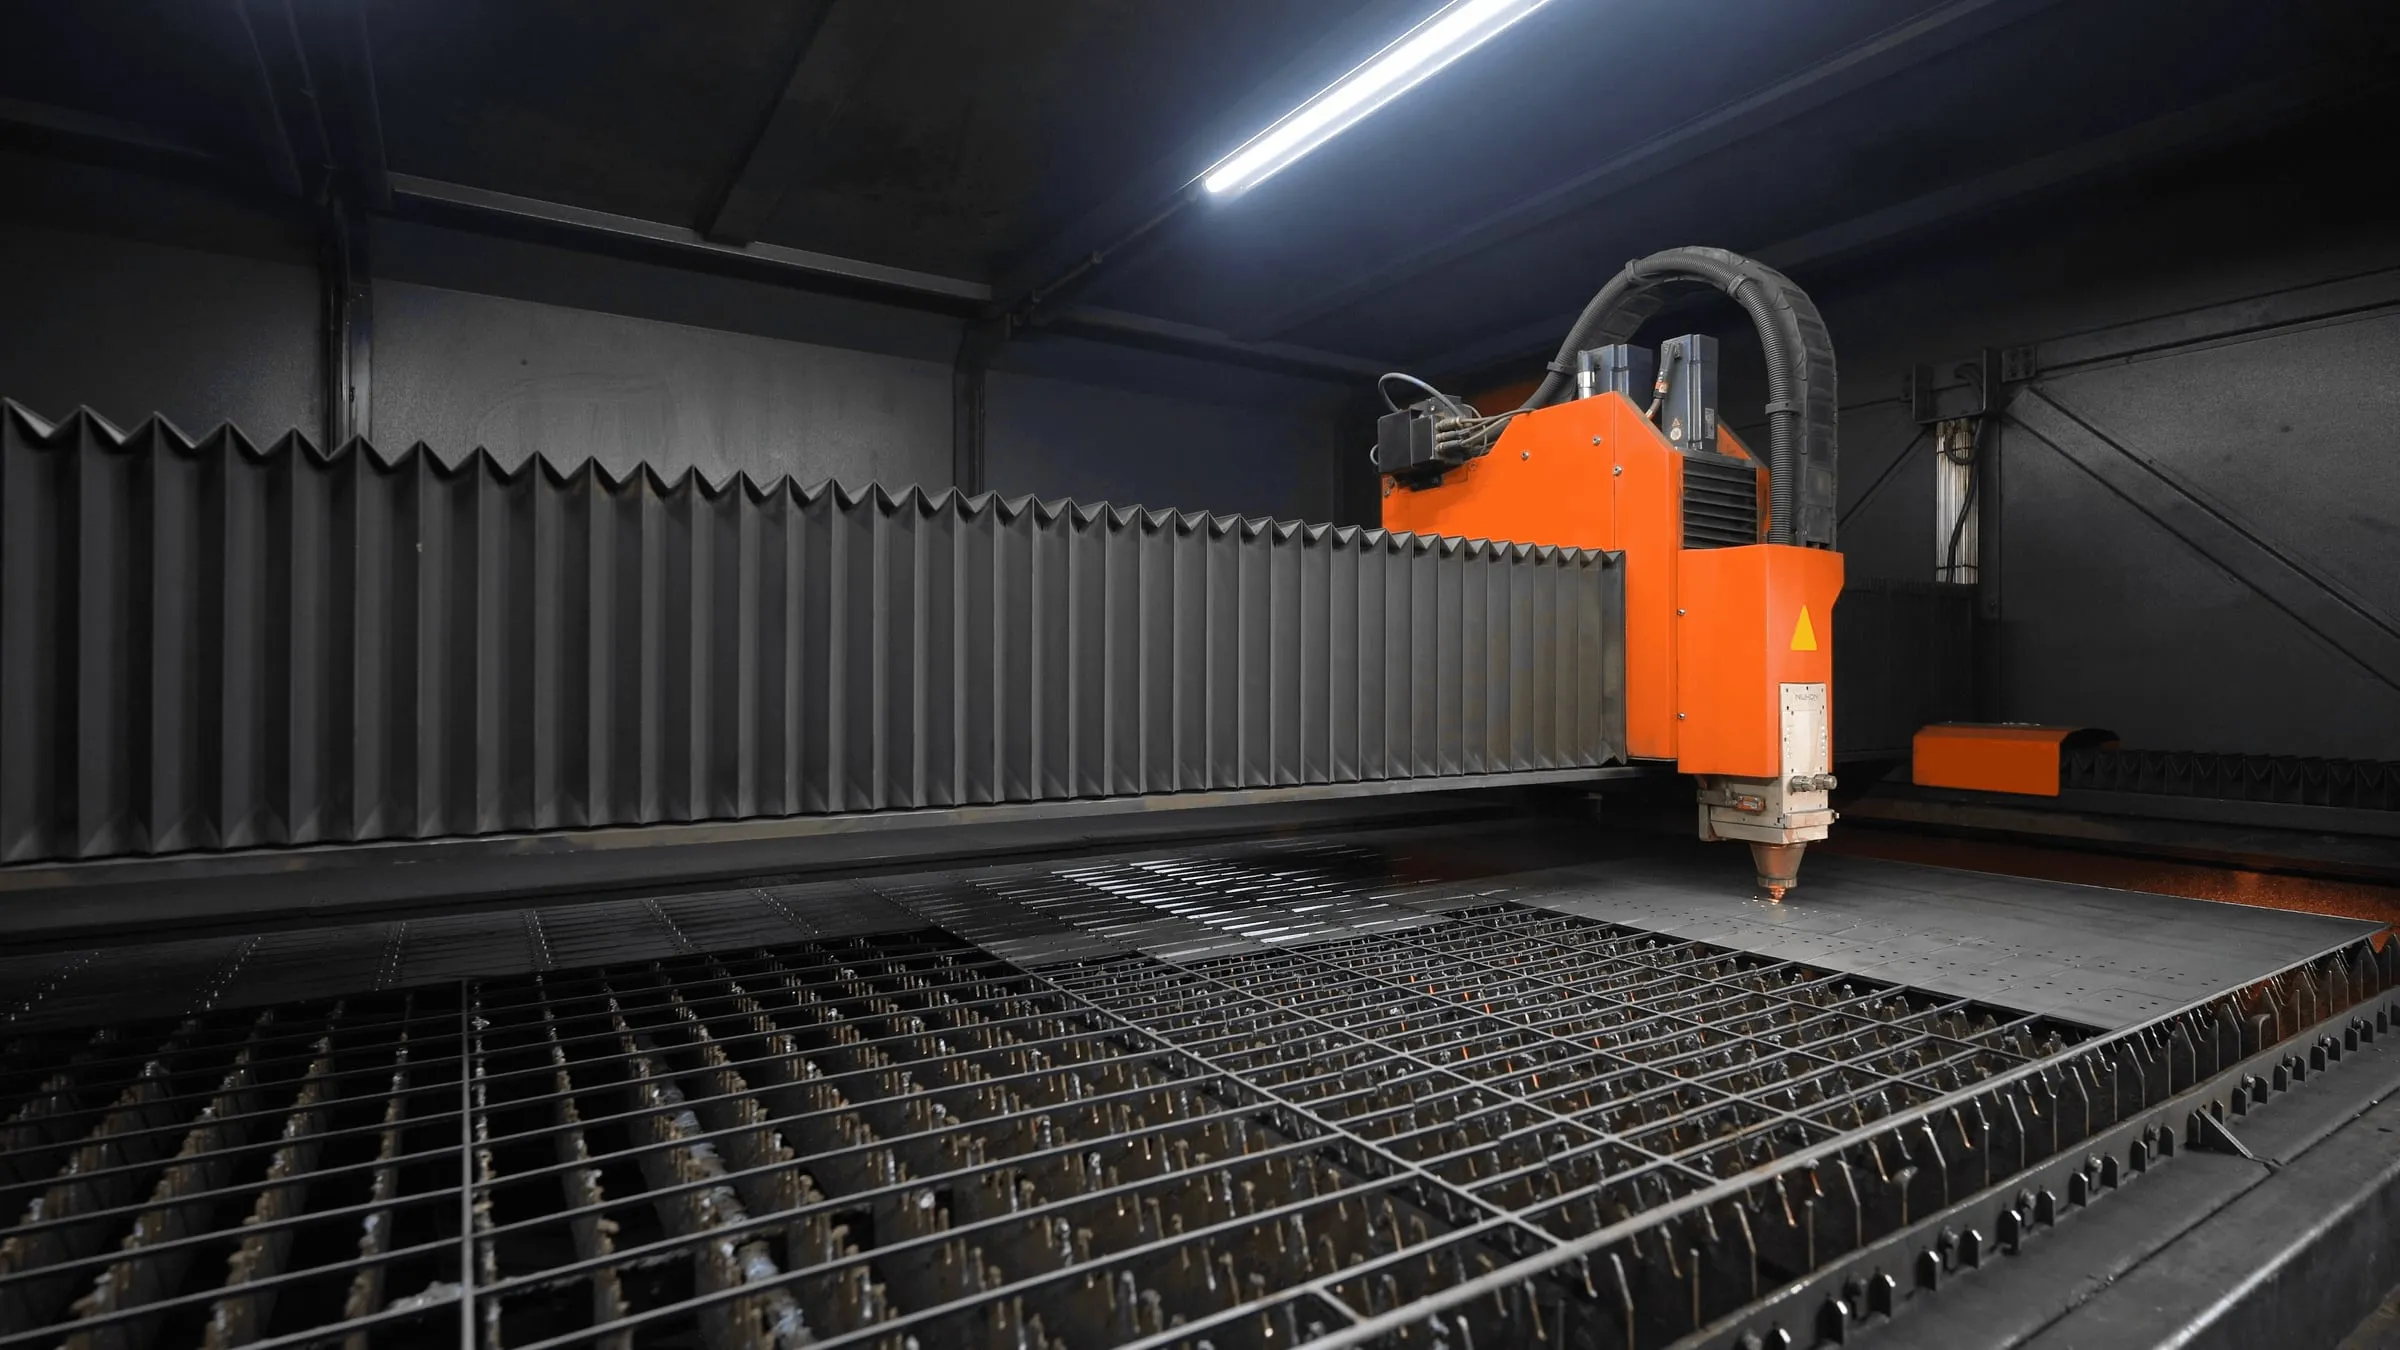
- Fibre laser cutting3–12 kW · up to 20 mm
- Turret punchingAmada · 200 kN
- CNC bendingup to 360 T
- Plate rolling3 m · Davi
- Plasma cutting330 A
- Shearingup to 16 mm
- Hydraulic pressing150 T
- MIG/MAG weldingPanasonic · up to 550 A
- MachiningLathe · drilling · grinding
- Shot blastingSurface preparation
- Pre-treatment9-tank line
- Powder coatingLight & heavy lines
- 2-pack liquid coating500 hr salt spray
- CMM inspectionWith scanner
- Final assemblyFixture-based
Select a process to see the machines behind it
[plant 01 · light fabrication]
Light fabrication plant
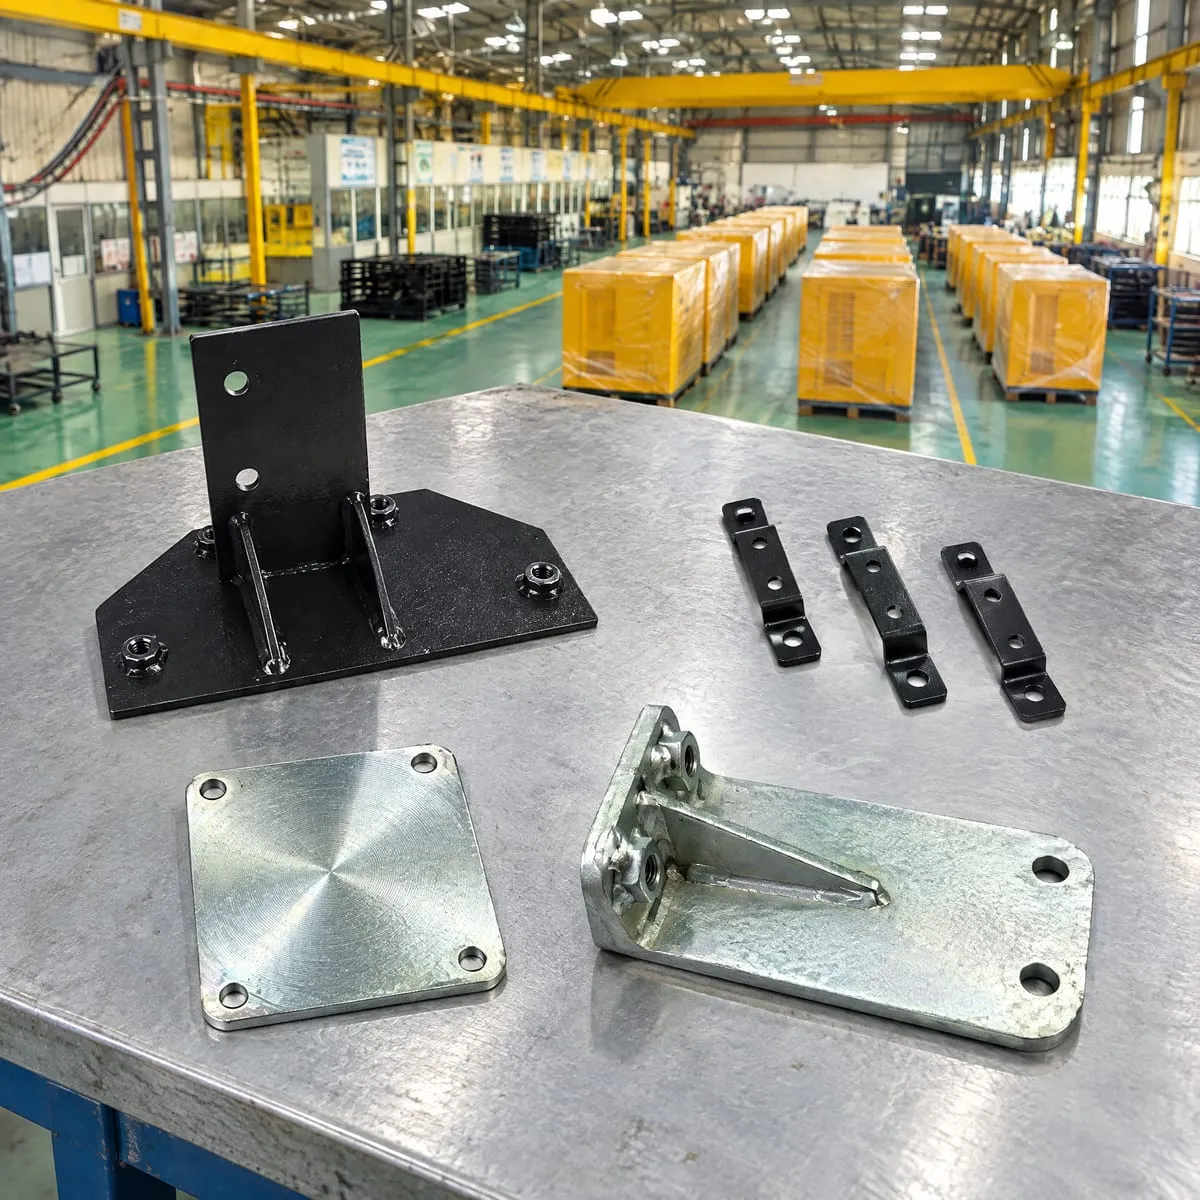
Sheet-metal work for genset and compressor canopies, base frames and brackets. Parts are cut, punched, bent, welded, pre-treated, powder coated and assembled in the same plant.
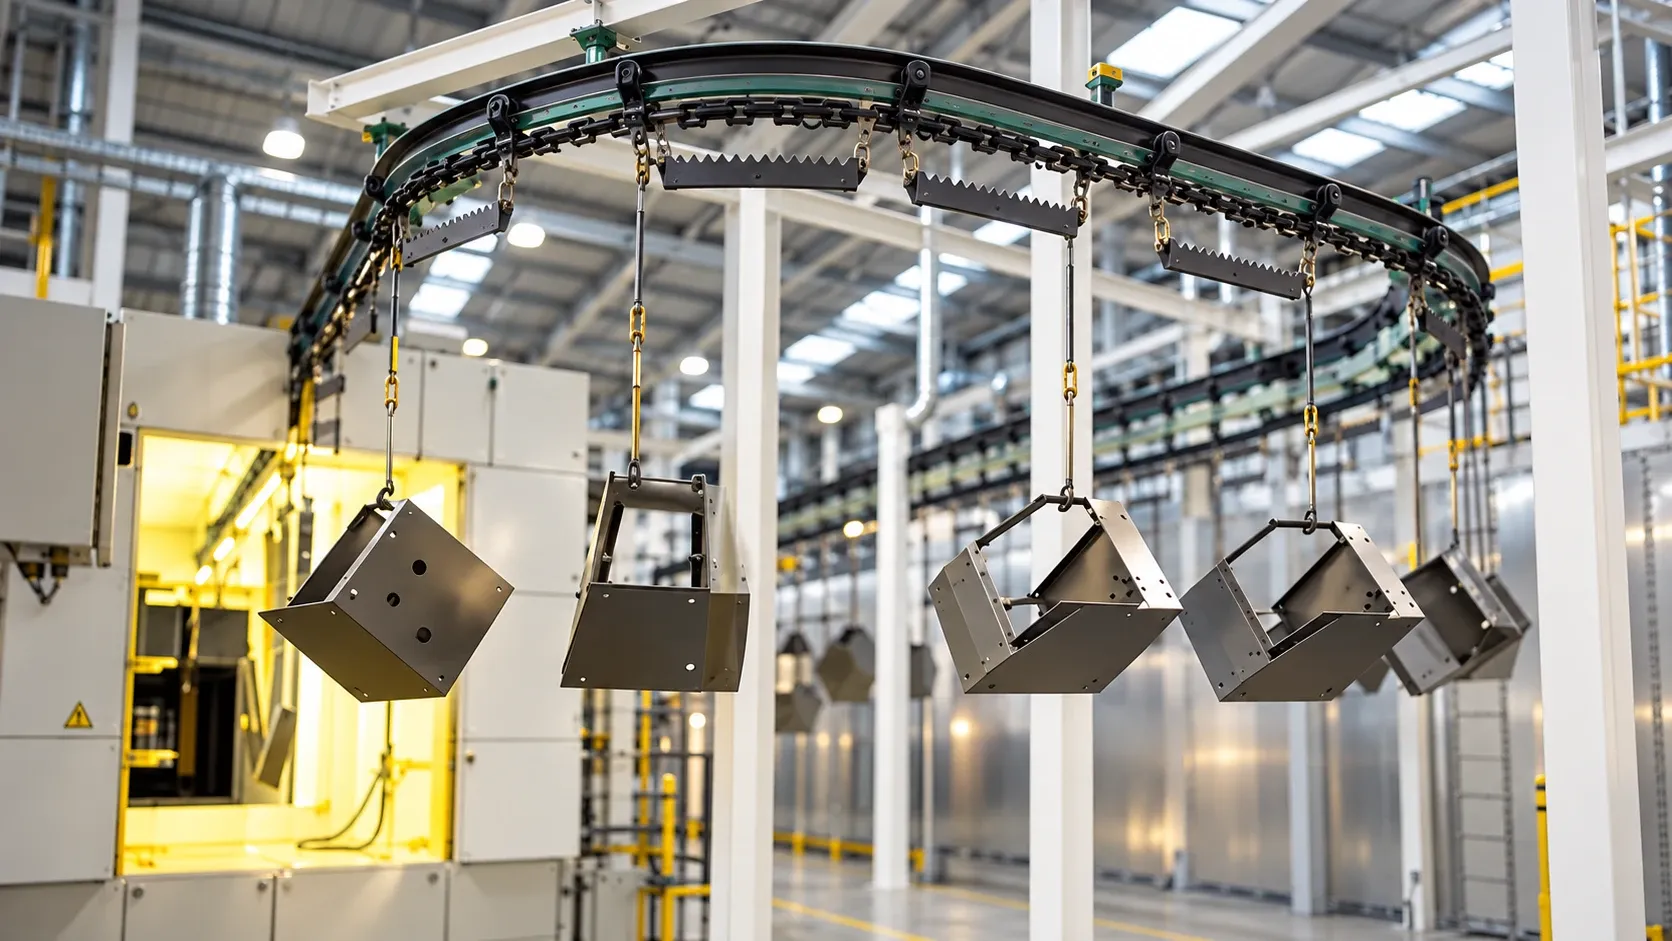
Fig. 01 / 06
[plant 01 · machines]
- Working area
- 6000 × 2000 mm
- Thickness
- up to 20 mm
- Drive
- Double gear, dual drive
- Build
- Fully covered body with pallet changer
Stainless, carbon, alloy, silicon and spring steel; aluminium; galvanised sheet and pickling board; copper and titanium.
- Punching force
- 200 kN
- X / Y axis
- 1250 / 1290 mm
- Max sheet thickness
- 3 mm
- Control
- AMNPC main drive
- Bending force
- 1000 kN (100 T)
- Bending length
- 3100 mm
- Axes
- 4+1 · X, Y1, Y2, R (TJS-90T)
- Crowning
- Hydraulic
3D programming with bending simulation, full-direction anti-collision, error alarms and German hydraulics.
- Capacity
- 100 T
- Axes
- 3+1
- Controller
- Cybelec 12 PS
- Max sheet width
- 3 m
CNC back gauge and full programming for efficient multi-bend mass production.
- Digital, fully controlled
- 550 A and 350 A
- MIG/MAG
- 400 A and 250 A
Digitally controlled pulse welding for clean, consistent joints from thin sheet to medium plate.
- Pre-treatment
- 9 tanks
- Powder coating
- Conveyorised line
- Salt spray
- 500 hr powder · 2000 hr with CED
- Assembly
- Fixture-based
Fig. 01 / 06
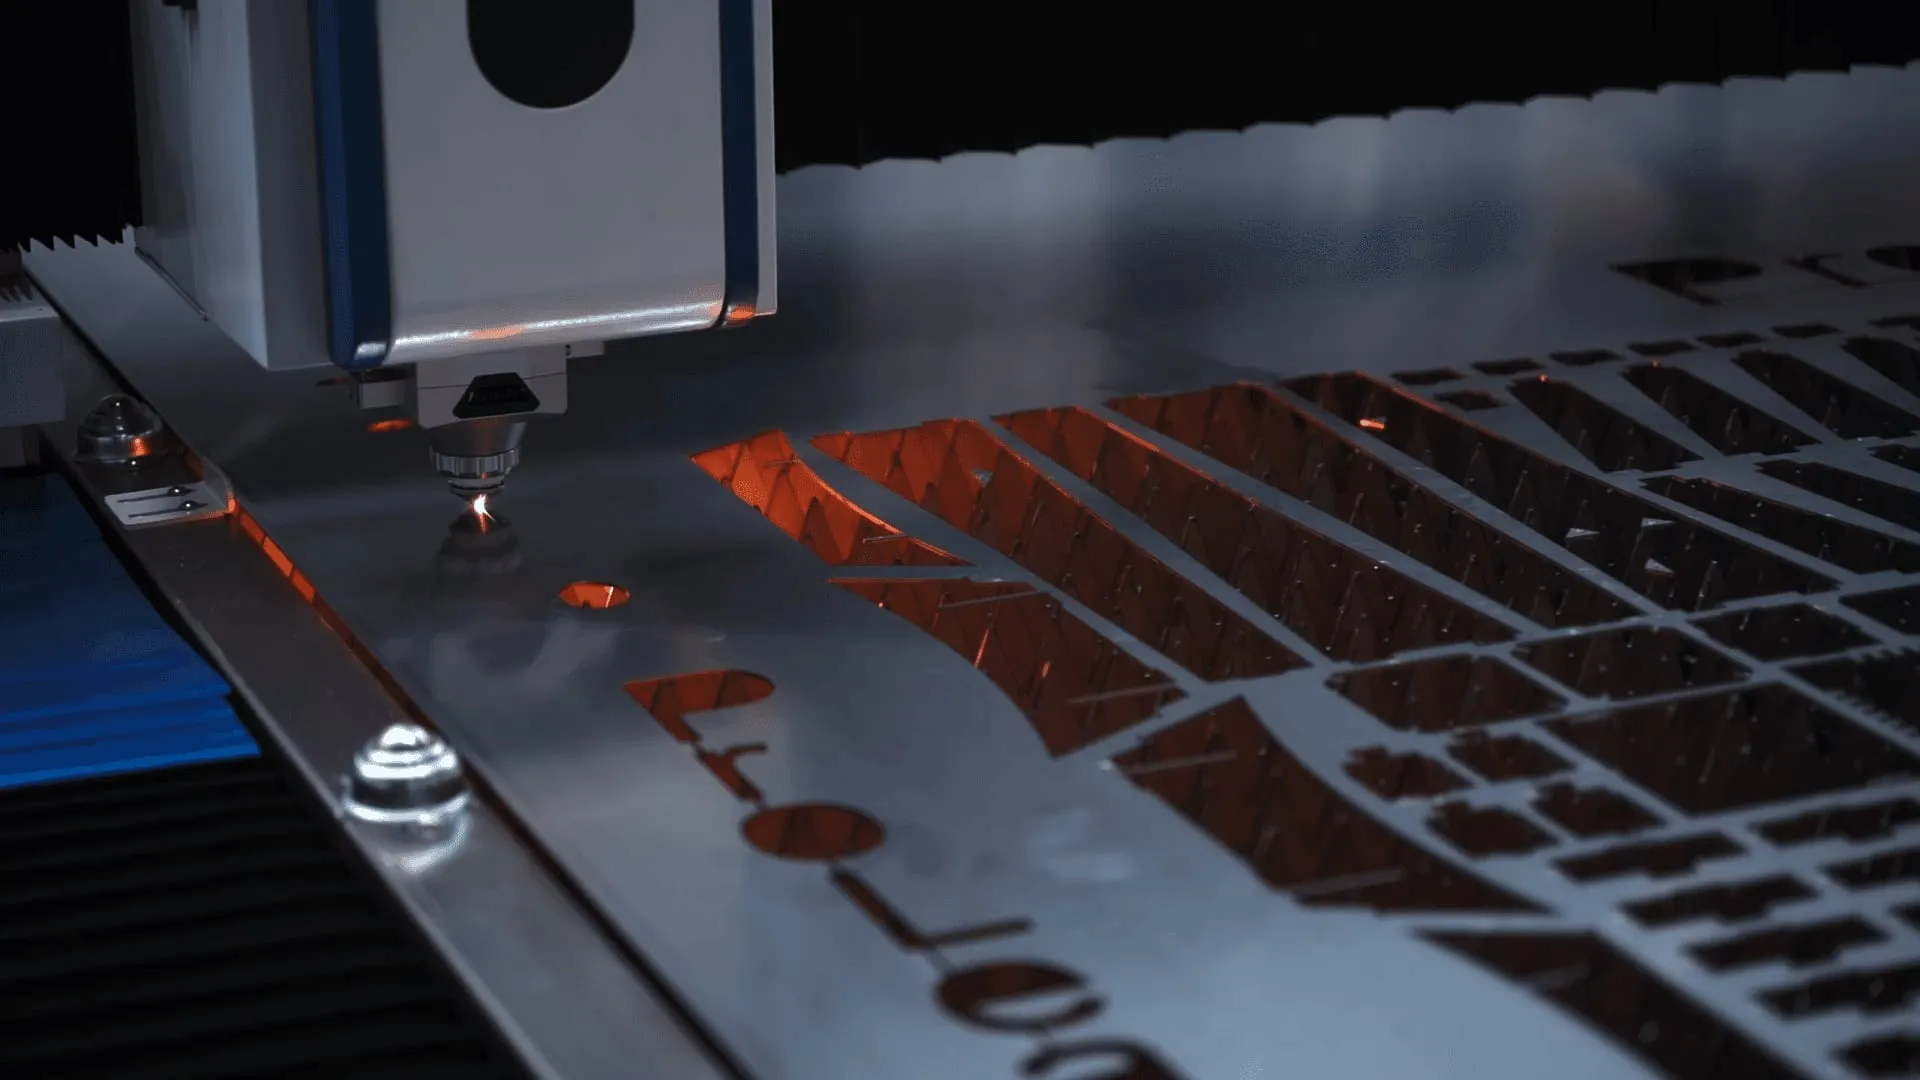
6 kWFibre laser sourceFibre laser cutting
RMI-C-6020 · 6 kW · Max Photonics source
- Working area
- 6000 × 2000 mm
- Thickness
- up to 20 mm
- Drive
- Double gear, dual drive
- Build
- Fully covered body with pallet changer
Stainless, carbon, alloy, silicon and spring steel; aluminium; galvanised sheet and pickling board; copper and titanium.
Fig. 02 / 06
200 kNPunching forceCNC turret punching
Amada Aries A255 NT
- Punching force
- 200 kN
- X / Y axis
- 1250 / 1290 mm
- Max sheet thickness
- 3 mm
- Control
- AMNPC main drive
Fig. 03 / 06
3100 mmBending lengthCNC press brake
JFY TPR8 100
- Bending force
- 1000 kN (100 T)
- Bending length
- 3100 mm
- Axes
- 4+1 · X, Y1, Y2, R (TJS-90T)
- Crowning
- Hydraulic
3D programming with bending simulation, full-direction anti-collision, error alarms and German hydraulics.
Fig. 04 / 06
100 TCapacityCNC press brake
RMI 3100
- Capacity
- 100 T
- Axes
- 3+1
- Controller
- Cybelec 12 PS
- Max sheet width
- 3 m
CNC back gauge and full programming for efficient multi-bend mass production.
Fig. 05 / 06
550 ADigital pulse weldingPulse MIG/MAG welding
Panasonic
- Digital, fully controlled
- 550 A and 350 A
- MIG/MAG
- 400 A and 250 A
Digitally controlled pulse welding for clean, consistent joints from thin sheet to medium plate.
Fig. 06 / 06
2000 hrSalt spray with CEDFinishing & assembly
Pre-treatment · powder coating · assembly
- Pre-treatment
- 9 tanks
- Powder coating
- Conveyorised line
- Salt spray
- 500 hr powder · 2000 hr with CED
- Assembly
- Fixture-based
[plant 02 · heavy fabrication]
Heavy fabrication plant
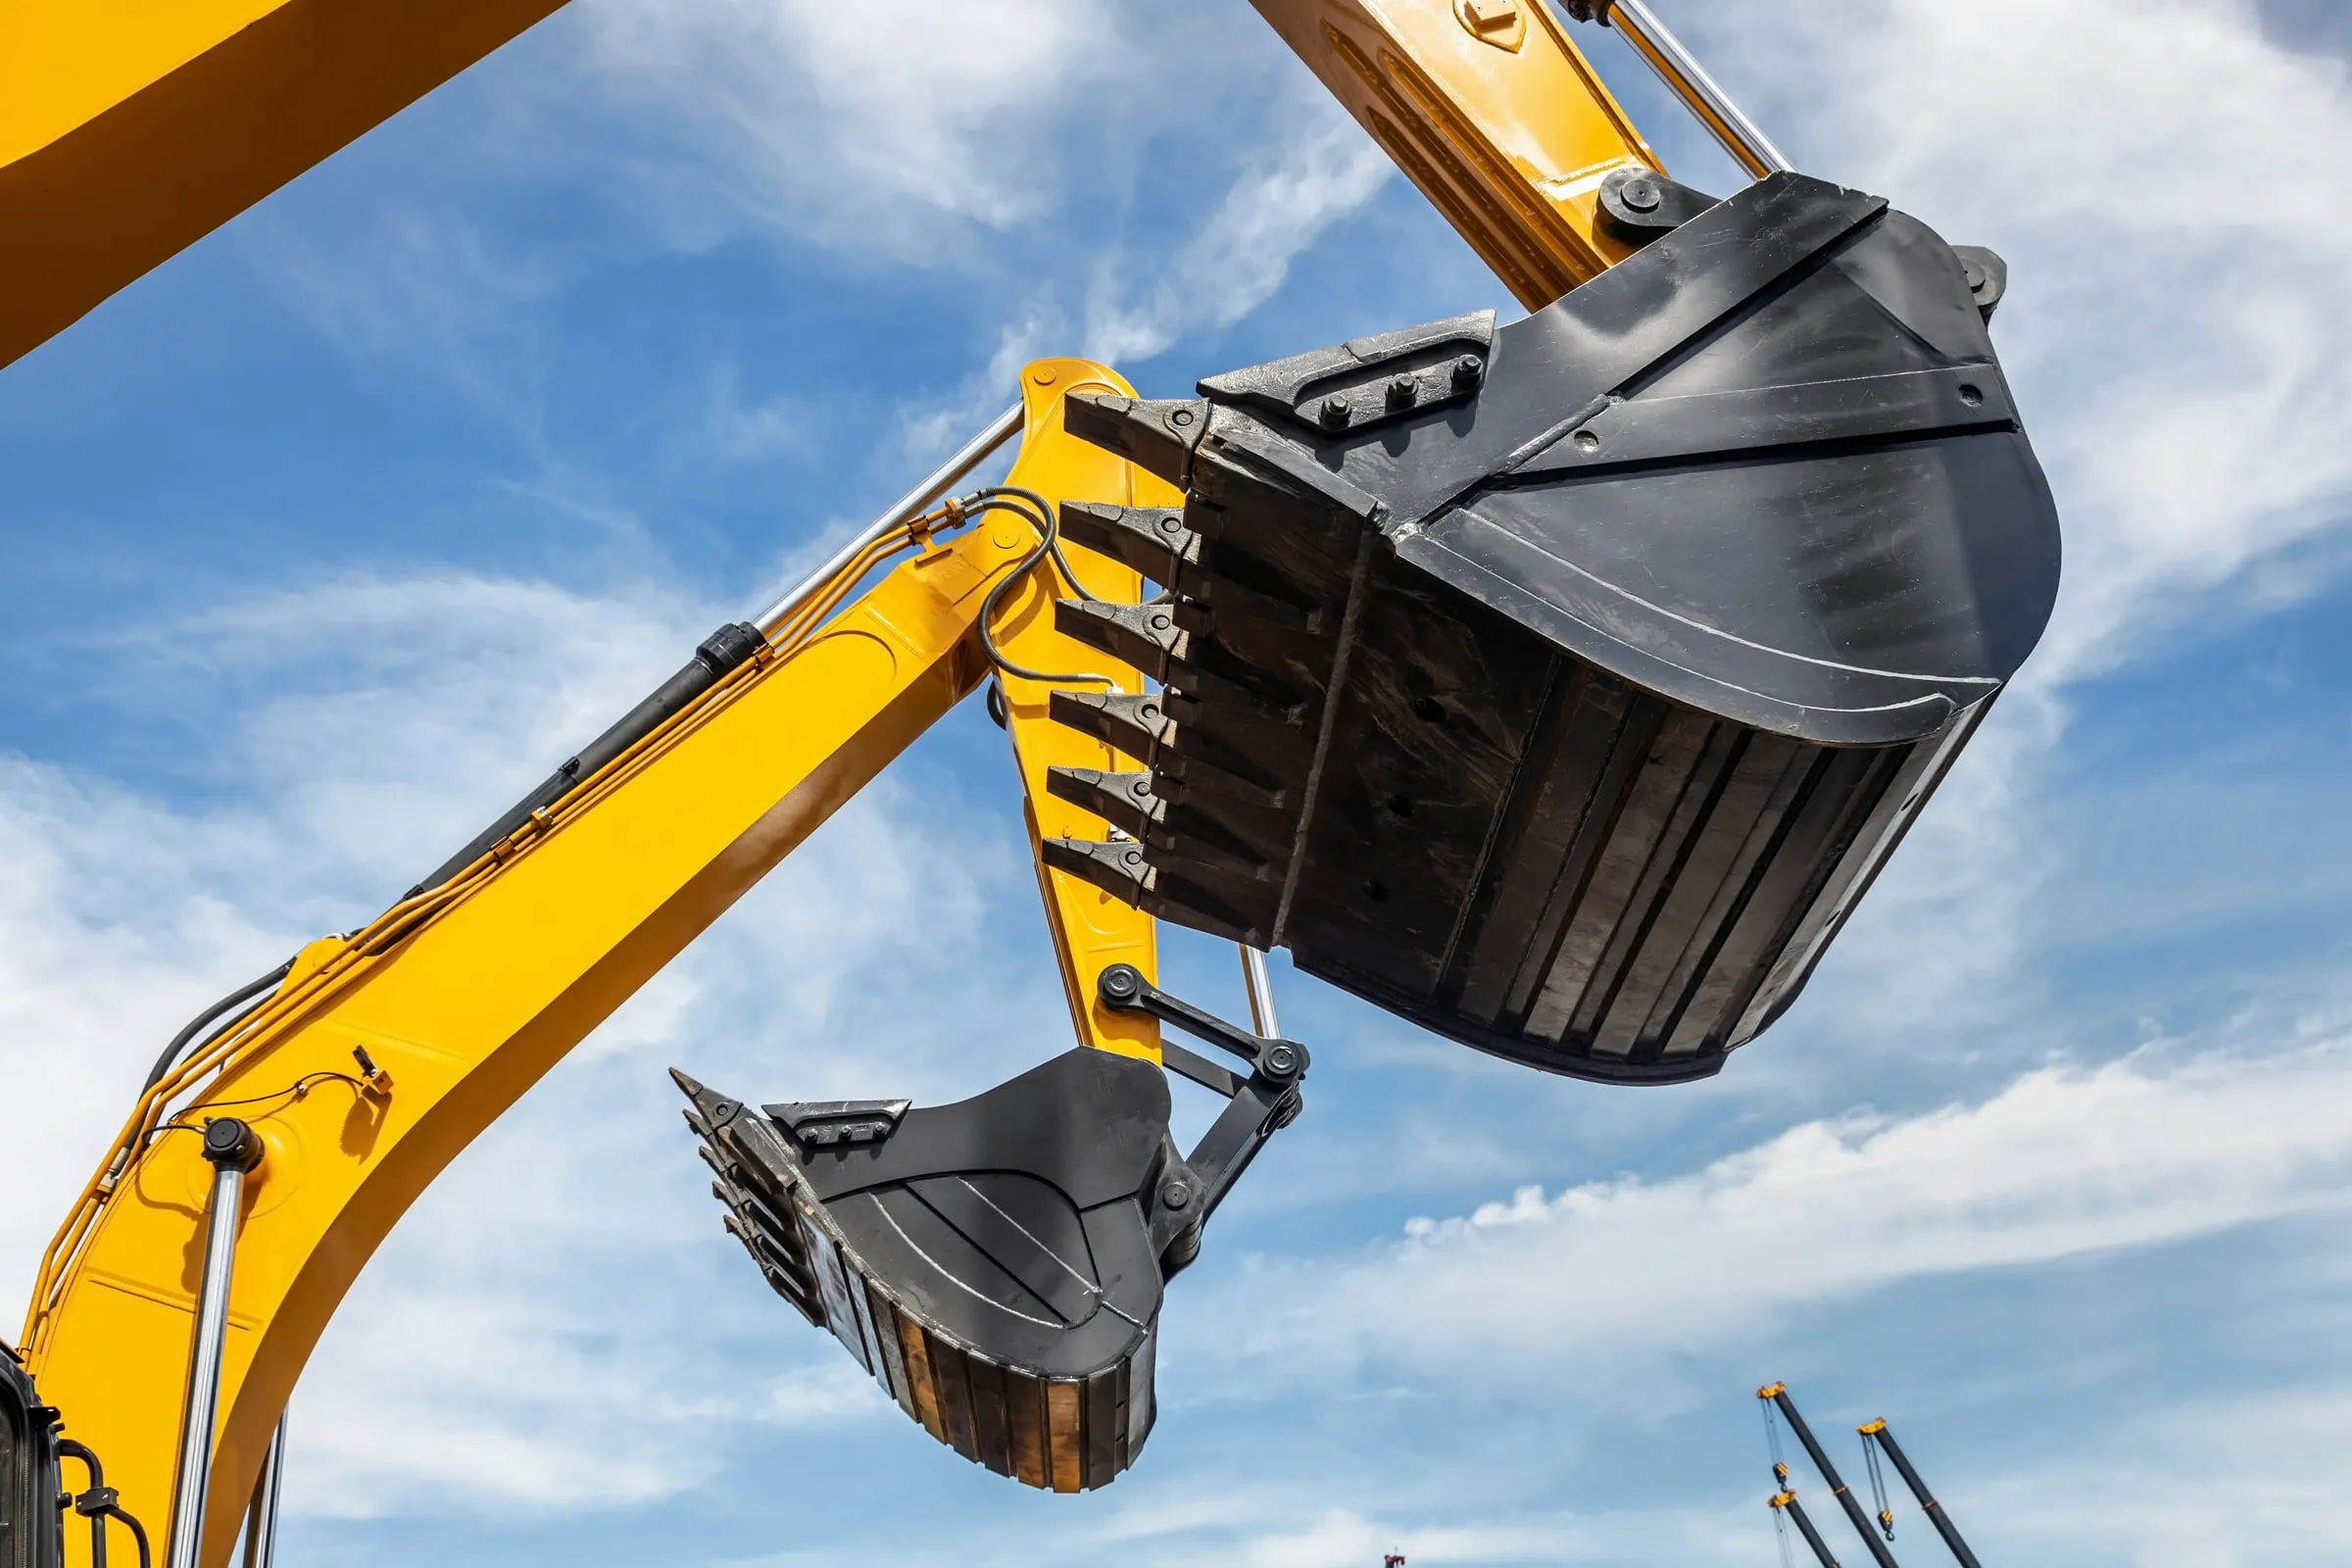
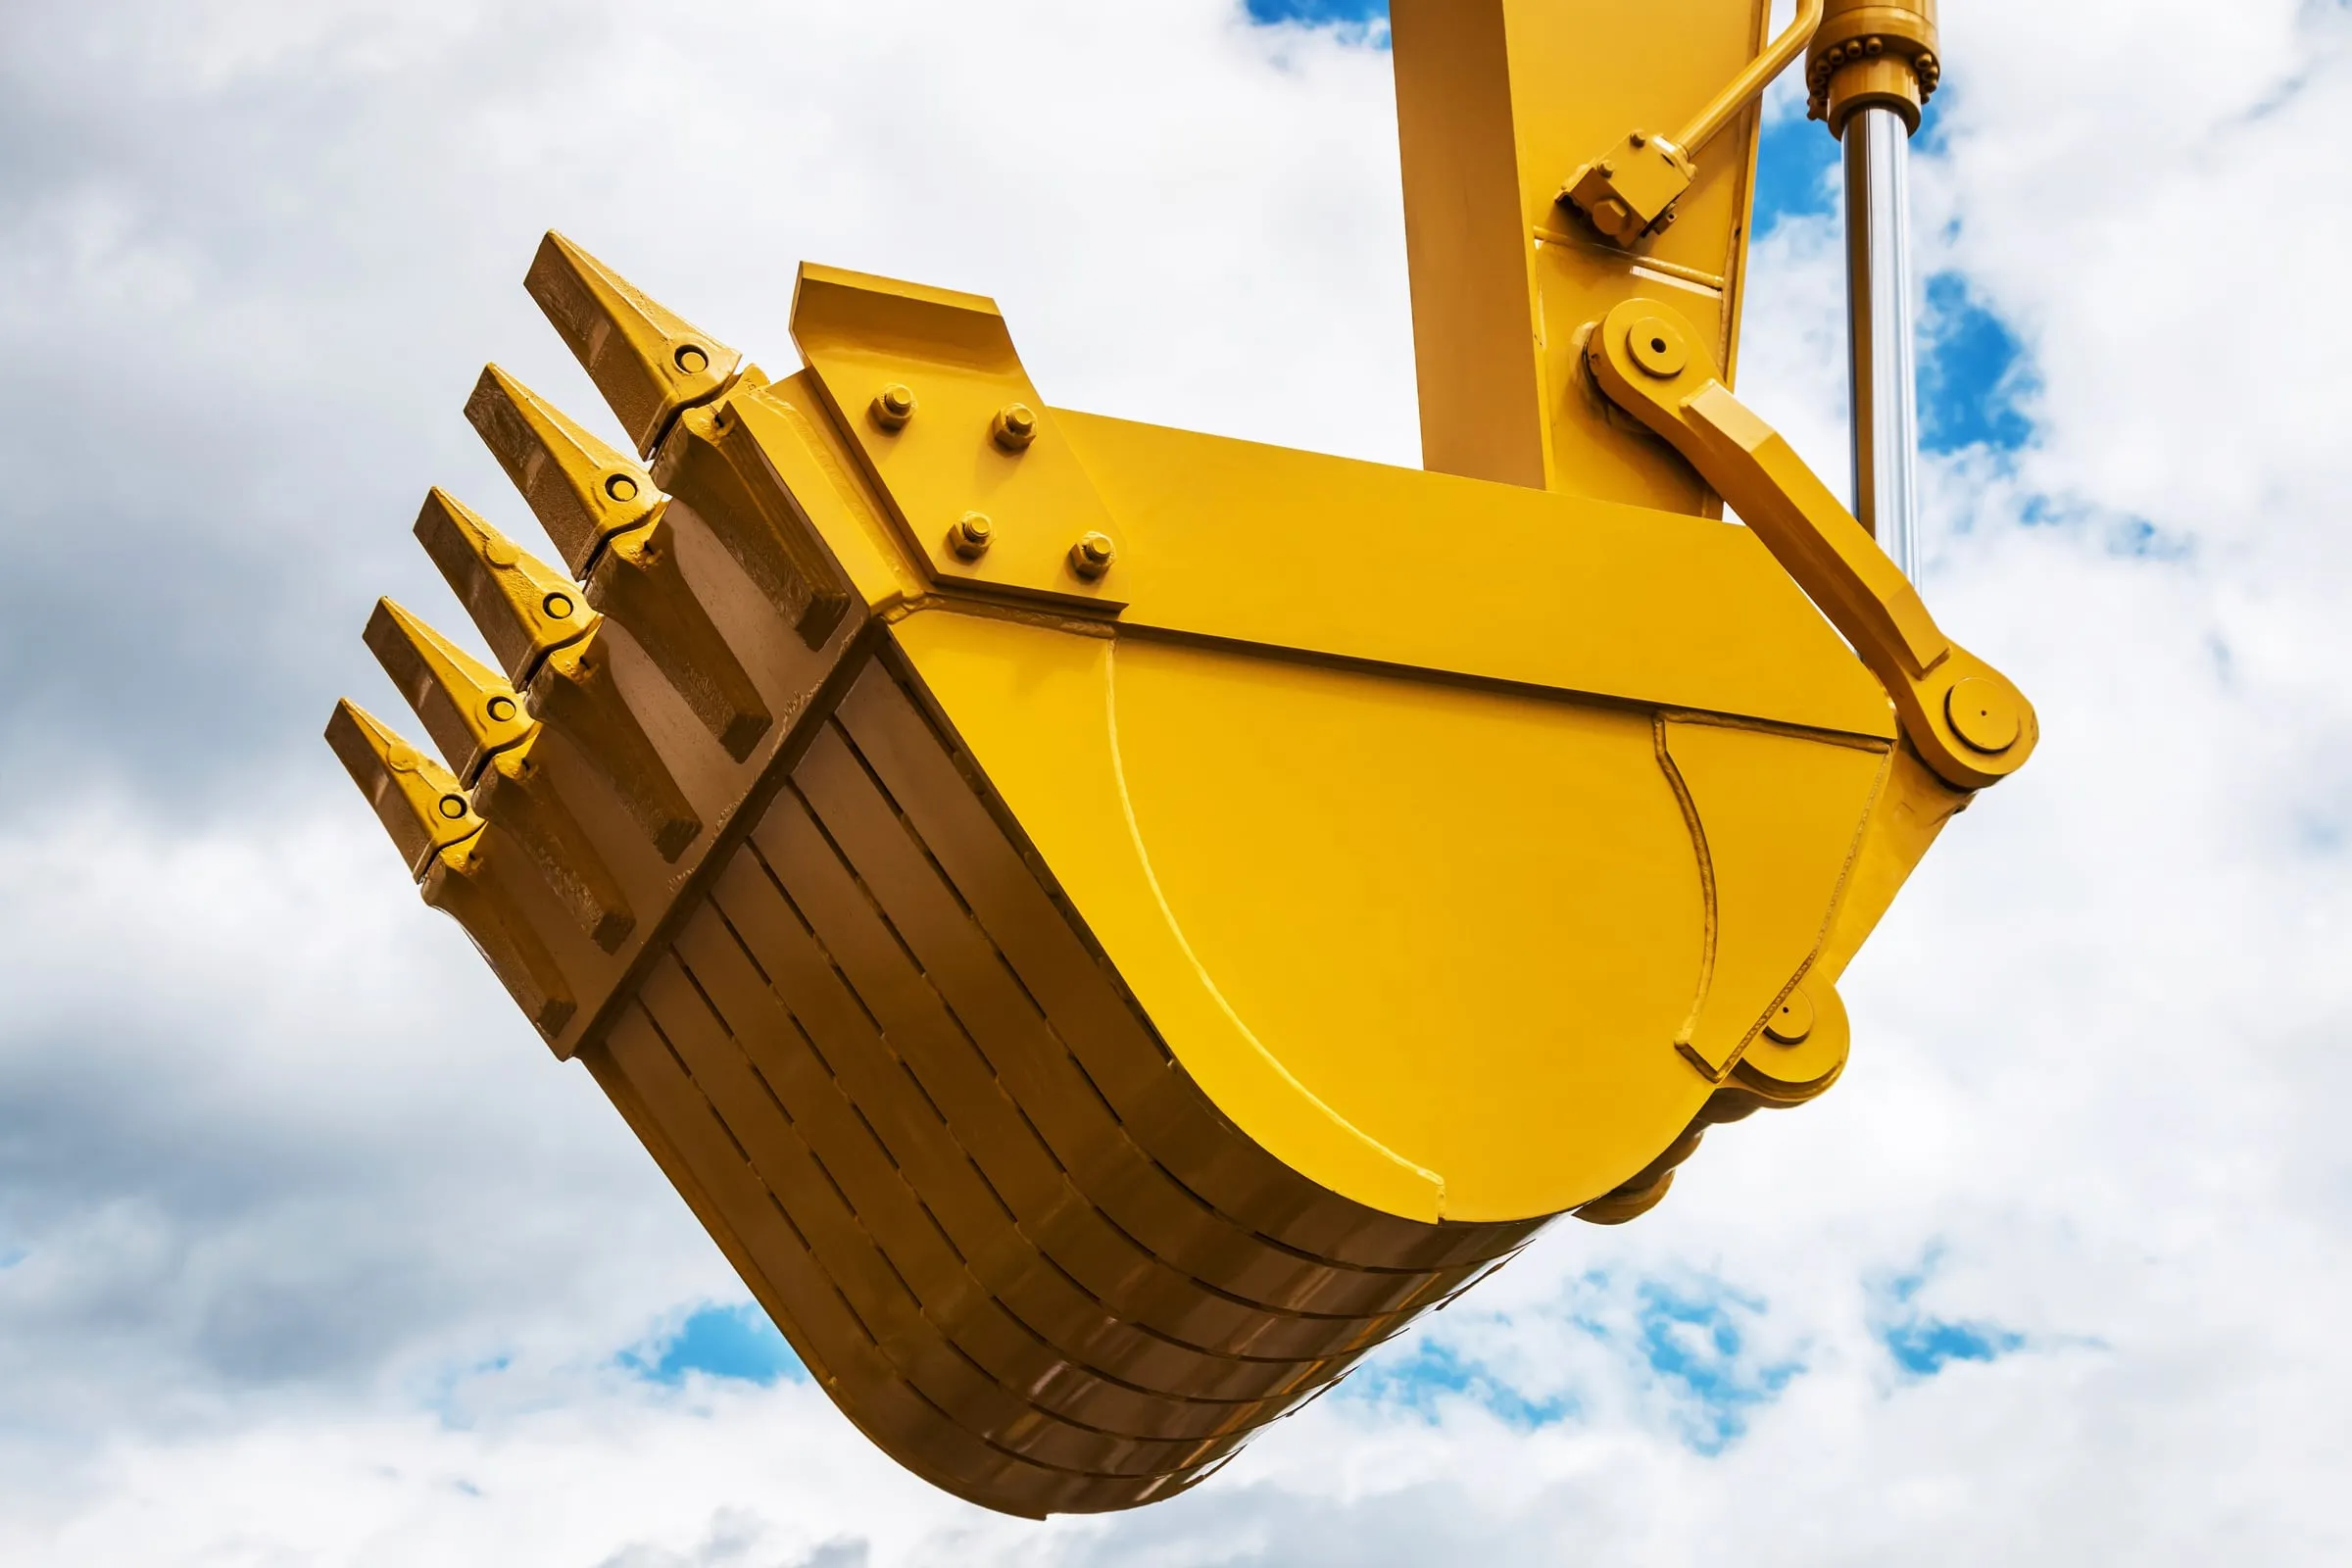
A dedicated plant for attachments: buckets, hanger brackets and heavy structures up to 2.5 tonnes, built from 10–40 mm plate in EN10355 SJ2 and Hardox 500.
- Lasers
- Trumpf 12 kW, Bystronic 3 kW
- Parts
- Bucket, bracket and structure profiles
- 360 T
- 4 m bed
- 225 T
- JFY
- Rolling width
- 3 m
- Plasma cutting
- 330 A
- Shearing
- up to 16 mm
- Capacity
- 150 T
- Welding sets
- 500 A
- Machining
- Lathe, drilling SPM, drill machine, MNTR
- Finishing
- Surface grinder
- Fitting
- Bush pressing, toe plate straightening
- Preparation
- Shot blasting
- Coating
- 2-pack liquid · 500 hr salt spray
- Powder
- Dedicated heavy-fabrication line
- Measurement
- Coordinate measuring machine
- Scanning
- 3D scanner
[Quality]
Measured, traced and certified at every stage
ISO
ISO 9001:2015 certified quality management across both plants.
CMM
Coordinate measuring machine with 3D scanner for first-article and in-process inspection.
100%
Traceability for every part back to its batch, date and time of manufacture.
0%
Rejection rate, with quality checks at every stage.
[location]
Palwal, Delhi NCR
Come and see a part go from flat sheet to finished assembly. Plant visits and supplier audits are welcome; tell us when you would like to come.
Plant address
Khasra No. 48/4,5,47/A, Patli KhurdPalwal, Haryana 121102Delhi NCR, India
mayank.chakarvarti@excava.co.inOpen in Google Maps[work with us]
Send us a drawing or a sample part
Tell us what you need and in what volume. We’ll quote it, build a prototype and test it, and start production only once you’ve approved the sample.